
Tungsten Carbide Dies, Punches & Stamping Tool Inserts | Precision Cold Heading & Forming Tooling
$29.86
Tungsten carbide punches, carbide cold heading dies, carbide stamping tool inserts, precision die bushings, carbide progressive die parts, Пуансоны из твердого сплава, Panda Carbide tooling China.
Product Overview:
Panda Carbide Technology CO., LTD. delivers zero-defect, micro-precision Tungsten Carbide Dies, Punches, and Stamping Tool Inserts engineered to keep your automated stamping and cold-heading lines running flawlessly.Manufactured from 100 % virgin micrograin tungsten carbide powders and consolidated using Overpressure HIP Sintering ( 1,450°C ), our precision carbide punches, heading dies, and progressive die components achieve an ISO 4499 A00 porosity rating. Engineered with extreme compressive strength ( 3,800 - 4,500 MPa ) and tight dimensional tolerances ( +/- 0.001 mm ), Panda Carbide tooling eliminates punch breaking, die splitting, and micro-galling under heavy cyclic impact loads ( >1,500 MPa ).
📩 Request a Free Quote
https://www.pandacarbide.com/contact-us
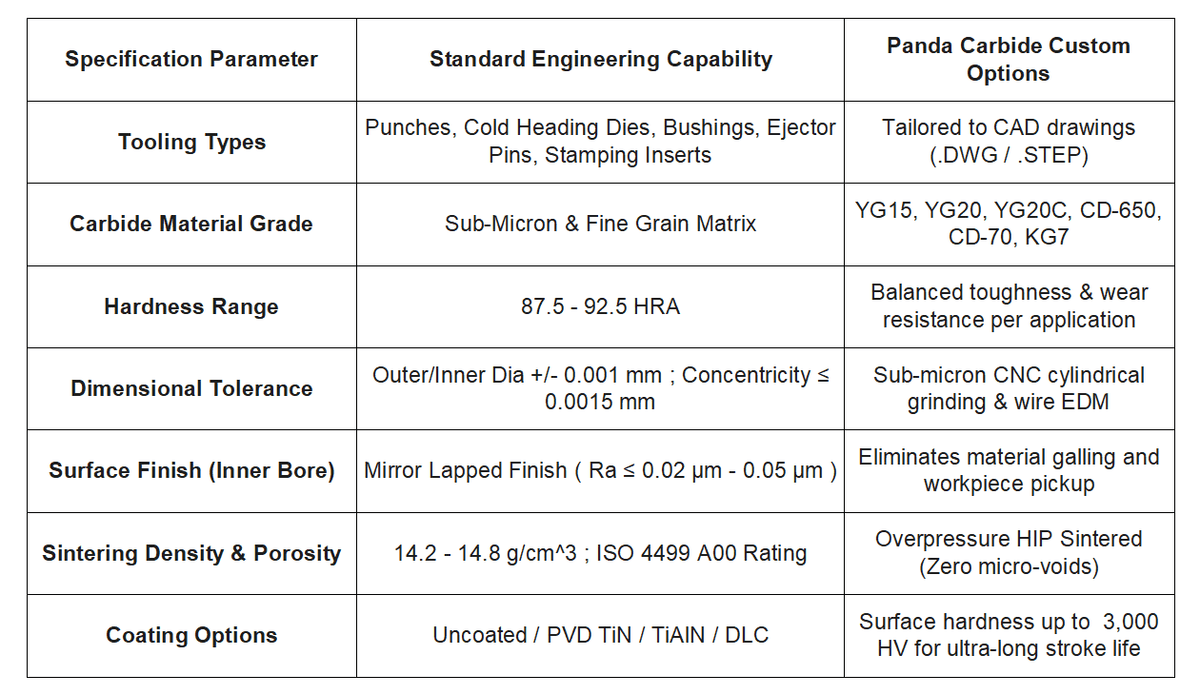
1. Technical Specifications & Custom Capabilities (Product Specs)
2. Material Recommendations & Carbide Grade Selection Guide
To prevent premature punch fracture, die cracking, or adhesive wear during high-speed stamping and cold forming, Panda Carbide offers specialized grade options:
For High-Impact Cold Heading & Fastener Forming (Nuts, Bolts, Rivets):
Recommended Grade: Panda YG20C / YG25 (Coarse/Medium Grain)
Key Advantage: High Cobalt binder content ( 15 % - 25 % ) delivers maximum fracture toughness ( K_IC ), absorbing heavy cyclic impact without die bursting or circumferential cracking.
For High-Speed Precision Stamping & Progressive Die Inserts (Connector Pins, Motor Lamination, Battery Cups):
Recommended Grade: Panda CD-650 / YG15 (Sub-Micron Grain 0.5 μm} - 0.8 μm )
Key Advantage: Ultra-high compressive strength ( >4,000 MPa ) and wear hardness ( 89.5 - 91.5 HRA ), maintaining razor-sharp punch edges and zero pitch drift over millions of strokes.
3. Core Technical Advantages & Engineering Features
100% Virgin Powder & Overpressure HIP Sintering: Consolidated under high argon pressure to eliminate microscopic voids, ensuring 100 % structural density and preventing sudden fatigue fracture during high-tonnage stamping.
Sub-Micron Concentricity & Mirror Polish: Precision CNC cylindrical and profile grinding achieves ≤ 0.001 mm concentricity and Ra ≤ 0.02 μm surface finish, reducing friction coefficients and preventing punch galling or sticking.
Pre-Stressed Shrink-Fit Casing Support: For heavy extrusion and cold-heading dies, custom tool steel (H13 / D2) casing surrounds the carbide core under optimized compressive pre-stress, counteracting radial hoop tension.
4. Target Industries & Machinery Compatibility
Primary Industries:
Automotive Component Manufacturing (Fasteners, Star Sockets, Engine Valve Tooling)
Precision Electronics & Connectors (Micro-punches, Terminal Stamping)
Fastener & Hardware Industry (Cold Heading Dies, Thread Rolling Accessories)
Lithium Battery & EV Manufacturing (Battery Can Deep Drawing Dies, Electrode Stamping)
Compatible Machinery:
Multi-Station Cold Headers (e.g., National, Sacma, Nedschroef)
High-Speed Precision Press Machines (e.g., Bruderer, Yamada Dobby, AIDA)
Powder Compacting & Hydraulic Press Systems
5. Technical Q&A
Q: How does sub-micron tungsten carbide improve the stroke life of precision stamping punches compared to high-speed steel (HSS)?
A: High-speed steel (HSS) punches deform and wear down rapidly under high-volume abrasive stamping, requiring frequent sharpening. Sub-micron tungsten carbide punches from Panda Carbide Technology CO., LTD. offer up to 10 X to 20 X longer stroke life due to superior hardness ( 89.5-92.5 HRA ) and high compressive strength ( >4,000 MPa ). Overpressure HIP sintering eliminates micro-porosity, preventing micro-edge chipping and maintaining exact punch dimensions over millions of continuous cycles.
Q: What geometry and surface finish parameters prevent workpiece galling in cold heading carbide die inserts?
A: Workpiece galling and sticking inside cold heading dies are primarily caused by microscopic surface rough spots and micro-voids under extreme forming pressure ( 1,500 - 2,000 MPa ). Panda Carbide resolves this by combining overpressure HIP sintering (ISO 4499 A00 porosity) with mirror inner-bore grinding ( Ra ≤ 0.02 μm ). This ultra-smooth, void-free contact surface minimizes friction, allows smooth part ejection, and drastically extends die fatigue life.
📩 6. Call to Action (CTA)
Looking to eliminate punch breakage, reduce machine downtime, and boost your production yield? Panda Carbide Technology CO., LTD. provides complete OEM/ODM customization based on your CAD drawings (.DWG / .STEP / .PDF).
Contact our engineering sales team for rapid B2B quotations and complimentary technical consultation!